Double Shot Molding for Prototypes and Production
Two shot injection molding combines two materials, colors or material properties into a single molded component. By forming both shots within a controlled molding process, manufacturers can create complex parts while reducing separate assembly, bonding and finishing operations.
RevPart provides double shot molding capabilities for engineers, product developers and entrepreneurs working from prototypes through production. The process can support rigid and soft-touch combinations, multicolor designs, integrated seals and other features that would otherwise require multiple components or manufacturing steps.
Double Shot Injection Molding at a Glance
Two shot injection molding, also called 2K injection molding or two-component molding, uses two injections of material to create one finished component. The first material forms the substrate. A second material is then molded onto or around selected areas of that substrate.
The process can simplify multi-material injection molding designs by integrating features that might otherwise need to be assembled afterward. It is commonly considered when a product needs multiple colors, varying material properties, ergonomic surfaces, seals or other integrated functional features.
For early-stage programs, the right process depends on the design, materials, quantities and testing goals. RevPart can help evaluate whether two-shot molding, conventional injection molding, overmolding or another manufacturing method makes the most sense for the project.
Why Consider Two Shot Injection Molding for an Early Program?
Functional prototypes become more useful when they accurately represent how the intended production part will perform. For products that ultimately require two materials, two shot injection molding can provide a more realistic way to evaluate fit, feel, material interaction and overall functionality.
Combining features into one molded component can also reduce part count and eliminate some manual assembly steps. Instead of molding separate components and joining them with adhesives, fasteners or secondary operations, the process can integrate both materials during manufacturing.
That does not mean two-shot tooling is automatically the lowest-cost choice for every prototype. Its tooling can be more complex than a single-shot mold. RevPart can help compare the upfront investment with expected quantities, assembly requirements and long-term production goals before tooling begins.
How Does the Double Shot Injection Molding Process Work?
Two shot injection molding uses a mold and machine configuration designed to expose the first molded section of the part to a second injection.
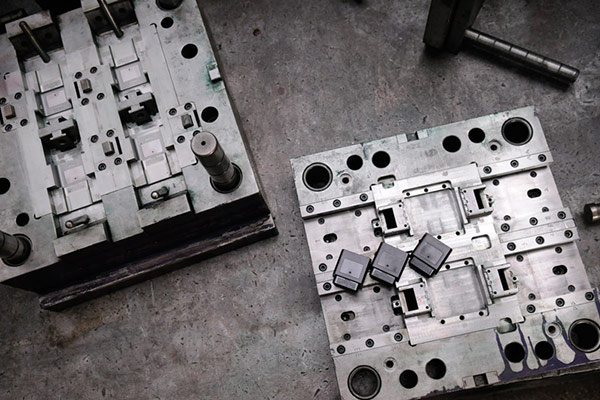
The exact setup depends on the mold and part geometry. RevPart’s plastic injection molding services include two-shot molding with a rotating platen, allowing the first shot to be repositioned for the next stage of molding.
Unlike standard single-shot injection molding, which typically fills the mold with one material during a cycle, the two-shot process must control two material flows and the relationship between them.
Two Shot Injection Molding Step by Step
First, the initial resin is injected into the first mold cavity. The material fills the required geometry and is allowed to cool enough to maintain its shape.
The first shot is then repositioned for the second operation. Depending on the machine and tooling configuration, this can involve mold or platen rotation or another controlled transfer method.
Next, the second material is injected into the appropriate portion of the mold. It flows against or around the first shot to create the desired secondary feature. After sufficient cooling, the completed part is ejected.
Quality evaluation may include dimensional inspection, visual review, verification of shot alignment and examination of the interface between materials. Functional testing can also be important when the second shot serves as a seal, grip, flexible feature or other performance-critical element.
Materials for Two Shot Injection Molding
Material selection is one of the most important decisions in two shot injection molding. Engineers may combine two rigid thermoplastics, use different colors of compatible resins or pair a rigid substrate with a softer thermoplastic elastomer.
Potential thermoplastics vary widely by application and may include materials such as ABS, polycarbonate, polypropylene and other engineering resins. TPE and TPU materials can be useful for grips, impact surfaces, seals and other flexible features.
Compatibility must be evaluated early. Some polymers can develop a strong bond under appropriate molding conditions, while others may require the part geometry to create a mechanical connection between the shots.
Liquid silicone rubber may also be considered when a project requires silicone performance characteristics. RevPart offers separate silicone rubber molding capabilities, including LSR and LIM. Because combining silicone and thermoplastic materials introduces additional tooling, temperature and bonding considerations, the proposed material system should be reviewed before assuming a two-shot approach is appropriate.
Designing Successful Two-Shot Parts
Good two shot injection molding begins with design for manufacturability. The mold must fill correctly during both shots while maintaining the position and integrity of the first molded section.
Uniform wall thickness can help manage filling, cooling and shrinkage. Appropriate draft makes it easier to release the finished component without damaging molded surfaces.
The interface between the materials deserves particular attention. When chemical adhesion alone is not sufficient, designers may incorporate undercuts, holes, grooves or other mechanical interlocks that allow the second material to physically lock onto the first.
Material shrinkage should also be considered. Two materials with significantly different shrink rates can create warping, dimensional changes or stress at the interface.
Gate locations, textures, cosmetic requirements and the relative mass of each shot should all be reviewed during mold design. Engaging the molding supplier before the design is finalized can identify these issues while changes are still relatively easy to make.
Tooling and Manufacturing Considerations
A two-shot mold is more complex than conventional single-shot tooling because it must manage two molding stages and maintain accurate alignment between them. That additional complexity can increase initial tooling costs.
Cycle time depends on factors such as material selection, part thickness, cooling requirements, shot size and how the part transitions between molding stages. Good process control is important because variations during the first shot can affect the second.
Tool maintenance also matters. Parting surfaces, gates, vents and alignment features should remain in good condition to control flash and preserve the relationship between both materials.
For tight-tolerance components, dimensional inspection can verify that the two shots remain correctly positioned relative to each other.
Two Shot Molding vs. Overmolding
Two shot molding vs. overmolding is a common decision during multi-material product development. Both processes can combine materials, but their manufacturing workflows differ.
Traditional overmolding typically creates a substrate first and then places it into another mold for the secondary material. This provides flexibility and can make sense for prototypes, lower quantities or material combinations that are not suited to an automated two-shot process.
Two shot injection molding integrates both shots into a coordinated molding operation. Although tooling and machine requirements may be more complex, the process can reduce manual handling and secondary assembly. Those efficiencies become increasingly valuable as production quantities rise.
There is no universal volume at which one option automatically becomes more economical. Part geometry, materials, tooling requirements, cycle time and labor all affect the comparison. RevPart can evaluate the complete application rather than selecting a process based on volume alone.
Applications for Multi-Material Injection Molding
Two shot injection molding can support products in automotive, medical, industrial and consumer markets. The technology is especially useful when two materials or colors need to remain precisely positioned within the same component.
Potential applications include:
- Soft-touch grips on rigid housings
- Buttons or control surfaces integrated into enclosures
- Seals and flexible edges
- Multicolor indicators or branded components
- Impact-resistant or vibration-dampening surfaces
- Components combining rigid structural areas with flexible features
- Medical device components requiring multiple material properties
For medical applications, material requirements should be established early based on the intended use and regulatory needs of the finished device. Requirements for documentation, packaging, sterilization or additional testing should also be identified before production planning is finalized.
Common Two-Shot Molding Problems
Several defects can occur when material, tooling or processing conditions are not well matched.
Flash can develop when material escapes around the mold parting line or interface. Mold condition, clamping, injection pressure and material flow may all contribute.
Weak bonding can occur when the two materials are not chemically compatible or when molding conditions do not support adhesion. Changing materials, adjusting process conditions or incorporating mechanical interlocks may resolve the issue.
Different shrink rates can also cause distortion or stress as the materials cool. Material selection and part geometry should therefore be evaluated as a complete system rather than designing each shot independently.
Trial runs and inspection before larger-scale production can help identify these issues while adjustments can still be made efficiently.
When Is Two Shot Injection Molding Cost-Effective?
Two shot injection molding is worth evaluating when eliminating assembly or consolidating components can offset the additional tooling investment.
It may be a strong option when:
- The part needs two colors or distinct material properties.
- Components would otherwise require bonding or manual assembly.
- Precise alignment between materials is important.
- The design benefits from integrated grips, seals or flexible features.
- Production volume can justify more sophisticated tooling.
- Product quality benefits from automating multiple molding operations.
- The program is expected to scale after prototype or validation stages.
If design flexibility and low initial quantities are the primary concerns, overmolding or another prototype method may be more practical. RevPart can provide DFM input to help identify the right approach before committing to tooling.
RevPart Two Shot Injection Molding Services
RevPart works with customers from early product development through short-run and production manufacturing. Our broader rapid prototyping services give product teams access to multiple manufacturing options as a design moves from concept to functional testing and production.
For suitable multi-material designs, RevPart offers two shot injection molding with a rotating platen as part of our injection molding capabilities. We can review CAD files, material requirements, quantities and functional goals to help determine whether this process fits your application.
Early DFM feedback is especially valuable for two-shot parts because decisions about materials, interfaces, wall thickness, gates and tooling can affect both performance and manufacturing cost.
Frequently Asked Questions About Double Shot Molding
The process molds one material first, repositions the initial shot and then injects a second material into another area of the mold. The result is a single component containing two molded materials, colors or material properties.
Many thermoplastics and elastomers can be used, but successful combinations depend on chemical compatibility, processing temperatures, shrinkage and desired bond strength. When materials do not naturally bond well, mechanical interlocks may be incorporated into the design.
Neither process is universally better. Overmolding can offer flexibility for prototypes and lower quantities, while two shot injection molding can provide efficient, repeatable production when quantities and part requirements justify the tooling. The best choice depends on the complete application.
Major factors include part size and complexity, mold construction, shot geometry, material requirements, cavity count, tolerances and the mechanism used to reposition the first shot.
Yes, when the design and tooling strategy support the required quantities. Planning for expected production needs early can reduce redesign and tooling changes as the program grows.
Get a Quote for Your Two-Shot Project
If your product requires two materials, multiple colors or integrated functional features, send RevPart your CAD files and project requirements for review. Our team can evaluate the design, discuss material and manufacturing options and provide DFM feedback before tooling begins.